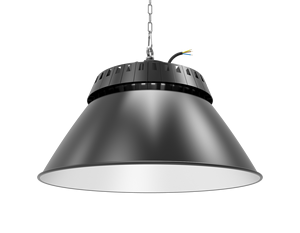
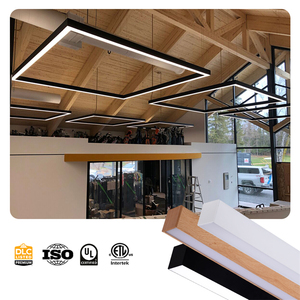
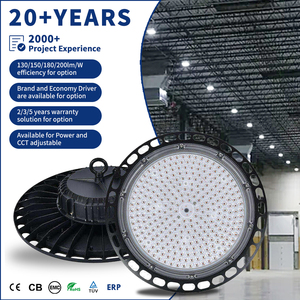
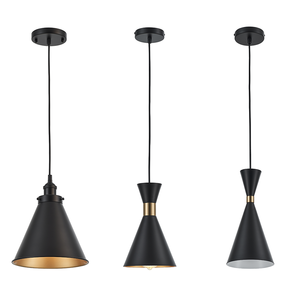
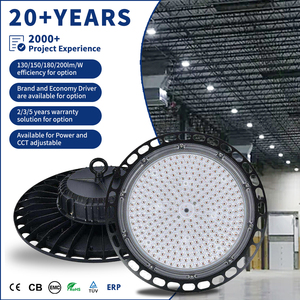
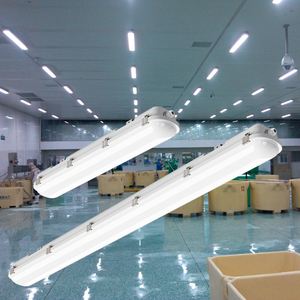
Explore our flagship OEM/ODM production portfolio—ranging from high-bay industrial luminaires and modular architectural linear suspended lights to hotel-grade commercial floor lamps and task luminaires engineered for intensive operational environments.
The global commercial floor lamp and decorative luminaire market is undergoing a seismic paradigm shift. Modern architectural specifications for hospitality, multi-family residential developments, senior living environments, and high-end commercial spaces no longer evaluate lighting purely through the lens of aesthetic design. Today’s global procurement directors, interior architects, and lighting specifiers demand an intricate convergence of high color rendering indexes (CRI ≥ 90, R9 > 50), modular mechanical assembly, thermal dissipation efficiency, energy compliance (Title 20/24, Energy Star), and robust international regulatory certifications (ETL, UL, CE, RoHS, IP-ratings).
When specifying floor lamps for large-scale projects, procurement teams face complex operational trade-offs between initial unit cost, freight footprint optimization (KD / Knock-Down packaging engineering), and structural longevity. A floor lamp deployed in a 5-star hotel guestroom or high-traffic commercial lounge must withstand thousands of duty cycles, continuous physical contact, cleaning chemical abrasion, and erratic electrical grid variances without flickering or mechanical wobble.
| Technical Parameter | Standard Mass-Market Floor Lamps | Architectural / Hospitality Grade (Majestic OEM) |
|---|---|---|
| Base Stability & Weighting | Stamping iron base (< 2.5 kg), risk of tipping over | Heavy-duty cast iron / weighted brass core (> 5.5 kg), tilt-tested > 15° |
| Optical Engine | Standard E26/E27 light bulb or raw LED tape | Custom Integrated LED / Edge-Lit LGP diffuser (SDCM < 3, Flicker-Free) |
| Color Rendering Index | CRI > 80, erratic R9 red rendering | CRI ≥ 90+ (CCT Tunable 2700K–5000K), R9 ≥ 50, TM-30 tested |
| Surface Finish Treatment | Single-layer spray paint (peels after 12 months) | 96-hr Salt-spray tested PVD electroplating / Powder-coat architectural finish |
| Switching & Smart Controls | Basic inline foot switch | ADA-compliant push button, rotary dimming, USB-C 18W / Qi Wireless Charging Base |
| Compliance Listing | Uncertified or basic CE mark | Fully ETL / UL Listed (UL 153 for portable luminaires, Damp location optional) |
As a leading custom lighting designer, manufacturer, and supply chain partner, Majestic Lighting operates at the intersection of aesthetic brilliance and rigorous structural engineering. Drawing on over 40 combined years of sourcing, design, and manufacturing expertise, our operational infrastructure eliminates the traditional friction points encountered by international buyers when sourcing floor lamps from China factories.
We maintain deep alignment with top global hospitality brand standards (Marriott, Hilton, IHG, Hyatt, Wyndham). Our floor lamp collections short-circuit approval bottlenecks by delivering spec-ready cutsheets, photometric IES files, and finish samples that match pre-approved brand criteria out of the box.
Through our unified family ecosystem, specifiers and purchasing agents can consolidate floor lamps, table lamps, wall sconces, vanity fixtures, and decorative backlit mirrors under a single spec-ready source. One contract, one dedicated project manager, and synchronized containerized delivery.
Electrical safety is paramount. Every floor lamp architecture undergoes rigorous third-party safety testing. Products carry clear ETL or UL marks (UL 153 for portable lamps), meeting local North American, European, and Middle Eastern electrical codes (ADA compliance, Title 20/24, Energy Star).
Whether starting from a designer’s napkin sketch, a 3D CAD rendering, or modifying a catalog model, our engineering team produces fully shop-drawn 2D/3D blueprints and physical prototypes in under 14 days for fast owner reviews.
Floor lamps are historically volumetric shipping nightmares. Our proprietary KD stem-threading and modular shade construction reduce master carton volume by up to 55%, dramatically lowering ocean freight cost per unit while passing ISTA 3A drop tests.
Commercial facilities require field serviceability. We design floor lamps with tool-less LED driver access, standardized socket modules, and provide a 5-year replacement parts availability window for uninterrupted hotel operations.
As commercial interiors evolve toward flexible work-lounge spaces, eco-conscious material transparency, and smart building management systems (BMS), floor lamp manufacturing is witnessing four primary technology convergence trends:
Traditional bulky fabric lamp shades are increasingly complemented or replaced by ultra-thin optical acrylic discs and edge-lit LED light engines. By employing laser-dotting technology on PMMA acrylic plates, modern floor lamps emit completely glare-free, uniform planar illumination (UGR < 19). This provides architectural sleekness while offering superior visual comfort for hotel guest reading nooks and executive lounges.
Inventory optimization is a major priority for global procurement distributors. Next-generation floor lamps produced in top China factories feature dip-switches integrated discreetly into the lamp housing. Procurement managers can switch color temperatures (2700K Warm White for evening ambience, 3000K Soft White for general lighting, and 4000K Cool Daylight for task reading) and adjust power output (e.g., 8W / 12W / 16W) on a single SKU, reducing inventory overhead by 66%.
The floor lamp is no longer just a static luminaire; it is a primary functional power hub. Floor lamp bases designed for hospitality and multi-family projects incorporate concealed high-speed USB-C Power Delivery (PD 18W–45W) ports alongside Qi wireless charging pads embedded under natural wood or polished marble base veneers. Additionally, Bluetooth Mesh and Zigbee 3.0 control modules enable seamless dimming integration into guestroom automation systems (GRMS).
Environmental, Social, and Governance (ESG) mandates require commercial buyers to scrutinize material origins. Leading China manufacturers are switching to 100% recyclable extruded 6063 aluminum alloys, low-VOC waterborne powder coating finishes, organic linen shades bonded with non-toxic bio-resins, and zero-plastic packaging made from recycled honeycomb cardboard.
Navigating the international lighting supply chain requires looking beyond basic FOB price tags. B2B buyers who achieve market dominance focus on Total Cost of Ownership (TCO), risk mitigation, and technical partner transparency.
Leading international buyers enforce strict three-tier quality control (QC) gates: Pre-Production Material Inspection (raw brass, aluminum gauge, driver lot testing), In-Line Assembly Audits (hi-pot electrical insulation test, ground continuity test), and Final Pre-Shipment Inspection (AQL 1.5/4.0 standard, 4-hour continuous burn-in test).
When FF&E budgets face pressure, expert OEM factories assist designers in value engineering (VE). By strategically adjusting internal structural wall thicknesses, substituting solid brass for heavy-gauge electroplated steel on non-tactile components, or standardizing driver footprints across multiple fixture types, projects can achieve 20-30% cost reductions without sacrificing aesthetic intent.
Unforeseen construction delays cost developers thousands of dollars daily. Top-tier manufacturers maintain strategic safety buffer stocks of universal LED drivers, shade frames, and electrical cords. This enables rapid prototype turnaround within 10 days and mass production completion within 30 to 45 days.
Comprehensive technical, compliance, and logistics answers for lighting procurement officers, interior designers, and hotel developers.
Partner with a proven OEM/ODM manufacturer trusted by over 70 global hotel brand programs. Request custom CAD shop drawings, factory-direct pricing, or physical material samples today.
Inquire Now